Induction Forging Equipment
Pre-heat billet, bar and round stock in seconds, not furnace cycles — so your press or extrusion line runs on your schedule, not the furnace's.
Weaken the material just enough to form it
Forging forms material — commonly steel, brass, or aluminum — that has been heated to the temperature at which resistance to deformation drops enough for a mechanical impact press, bending machine, or hydraulic extrusion press to shape it. Stock typically starts as round, square (billet), or bar material.
An induction pre-heat stage sits ahead of that forming step, bringing the stock to temperature directly and consistently, part after part, instead of soaking a batch in a furnace and hoping for even heat through the cross-section.
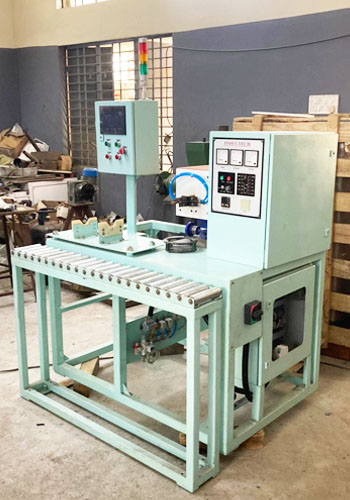
Eight reasons forging shops switch from open furnaces
- Superior quality and process control, part to part
- Shorter heating times with minimal surface oxidation/scale
- Precise, repeatable temperature control
- No furnace pre-heat or maintenance downtime
- Reduced labor through automation-ready operation
- Heat directed to one specific zone for single-area forming
Common questions about this process
How much faster is induction pre-heat than a furnace?
Induction heats the workpiece directly through electromagnetic coupling, so stock reaches forging temperature in seconds rather than the extended soak time a furnace batch needs, with no furnace warm-up or cooldown between runs.
Does induction forging cause less material loss?
Yes. Shorter heating times mean less time at high temperature for oxide scale to form, which reduces surface oxidation and the material loss that comes with open-furnace heating.
What stock shapes can be pre-heated with induction?
Round, square (billet), and bar stock are the common starting shapes, sized to the coil before being formed on a mechanical impact press, bending machine, or hydraulic extrusion press.
Can induction pre-heat integrate into an existing press line?
Yes. Because the coil heats a specific zone in seconds, it fits directly ahead of a press or extrusion line rather than running as a separate, disconnected furnace step.
Running a press or extrusion line?
Tell us your stock size and cycle time — we'll size the pre-heat coil to match your line speed.